Engineering · Surface Finishes
Surface finish reference.
A ladder from rough cast to optical-quality polish, with the processes that get you there and the cost implications of each step. Read this before tightening the surface callout.
Spec only what you need
Surface finish is a cost lever — not a default.
Machined lay · macro
Directional tool marks under raking light
- Ra 32 µin = 0.8 µm
- µin / µm
- ASME B46.1
Surface finish callouts are one of the easiest places to overspend. Many drawings inherit a 32 µin Ra default from an old template and apply it everywhere — including faces that will be hidden inside an assembly. Tighten only what serves a function: sealing, mating, optical, fatigue, or appearance.
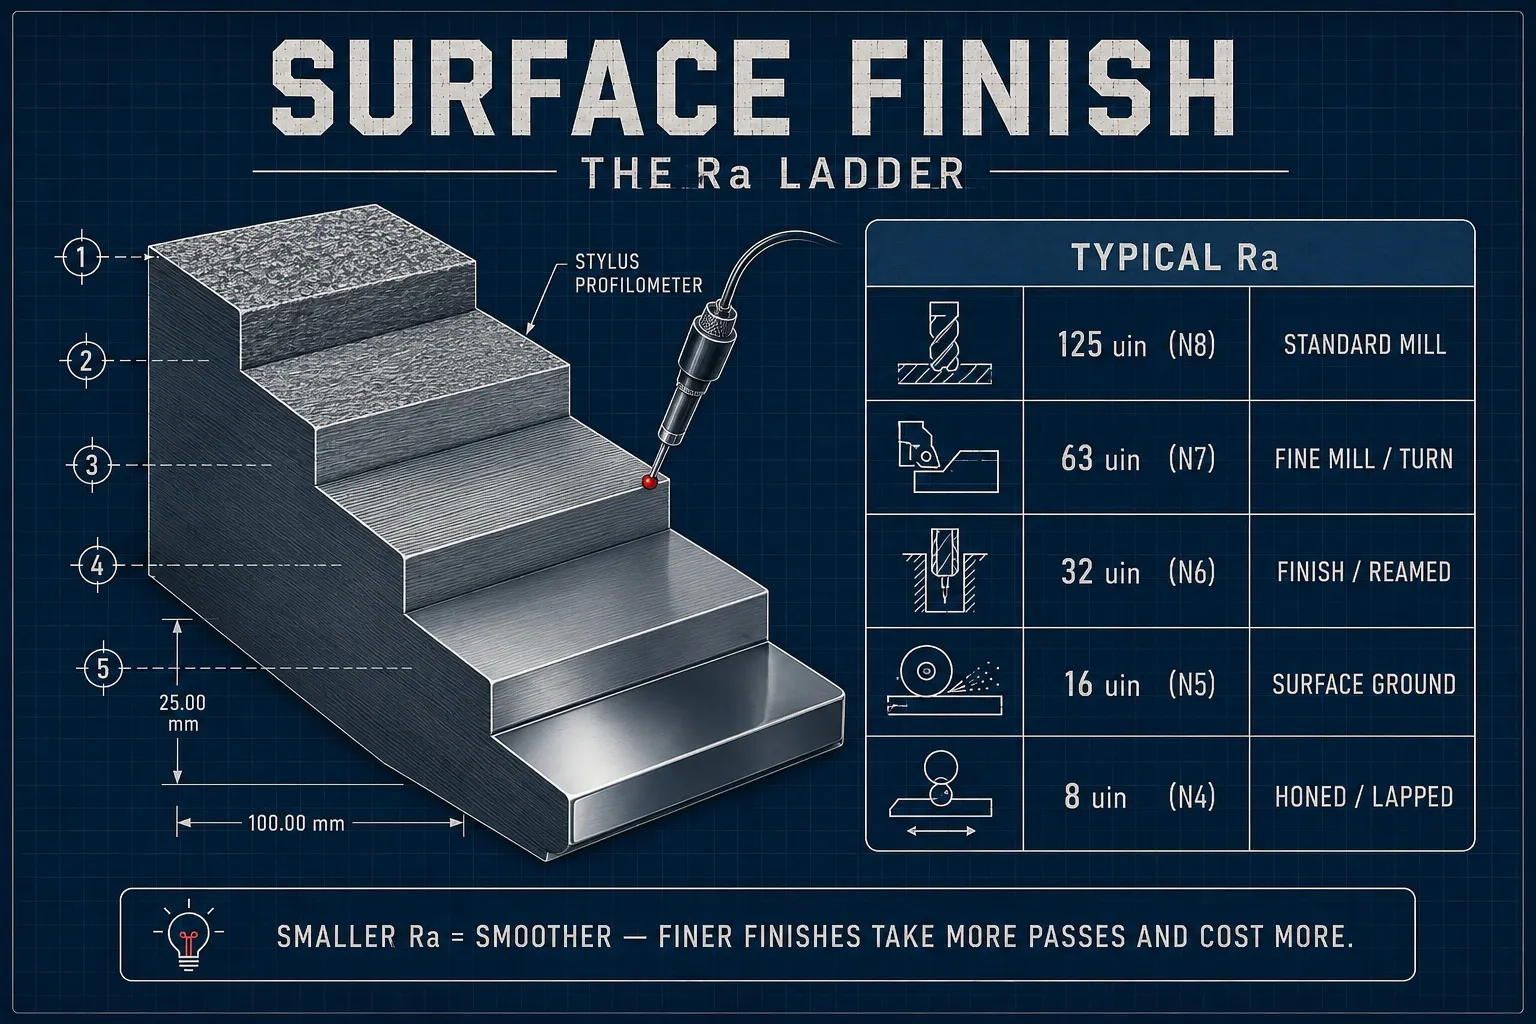
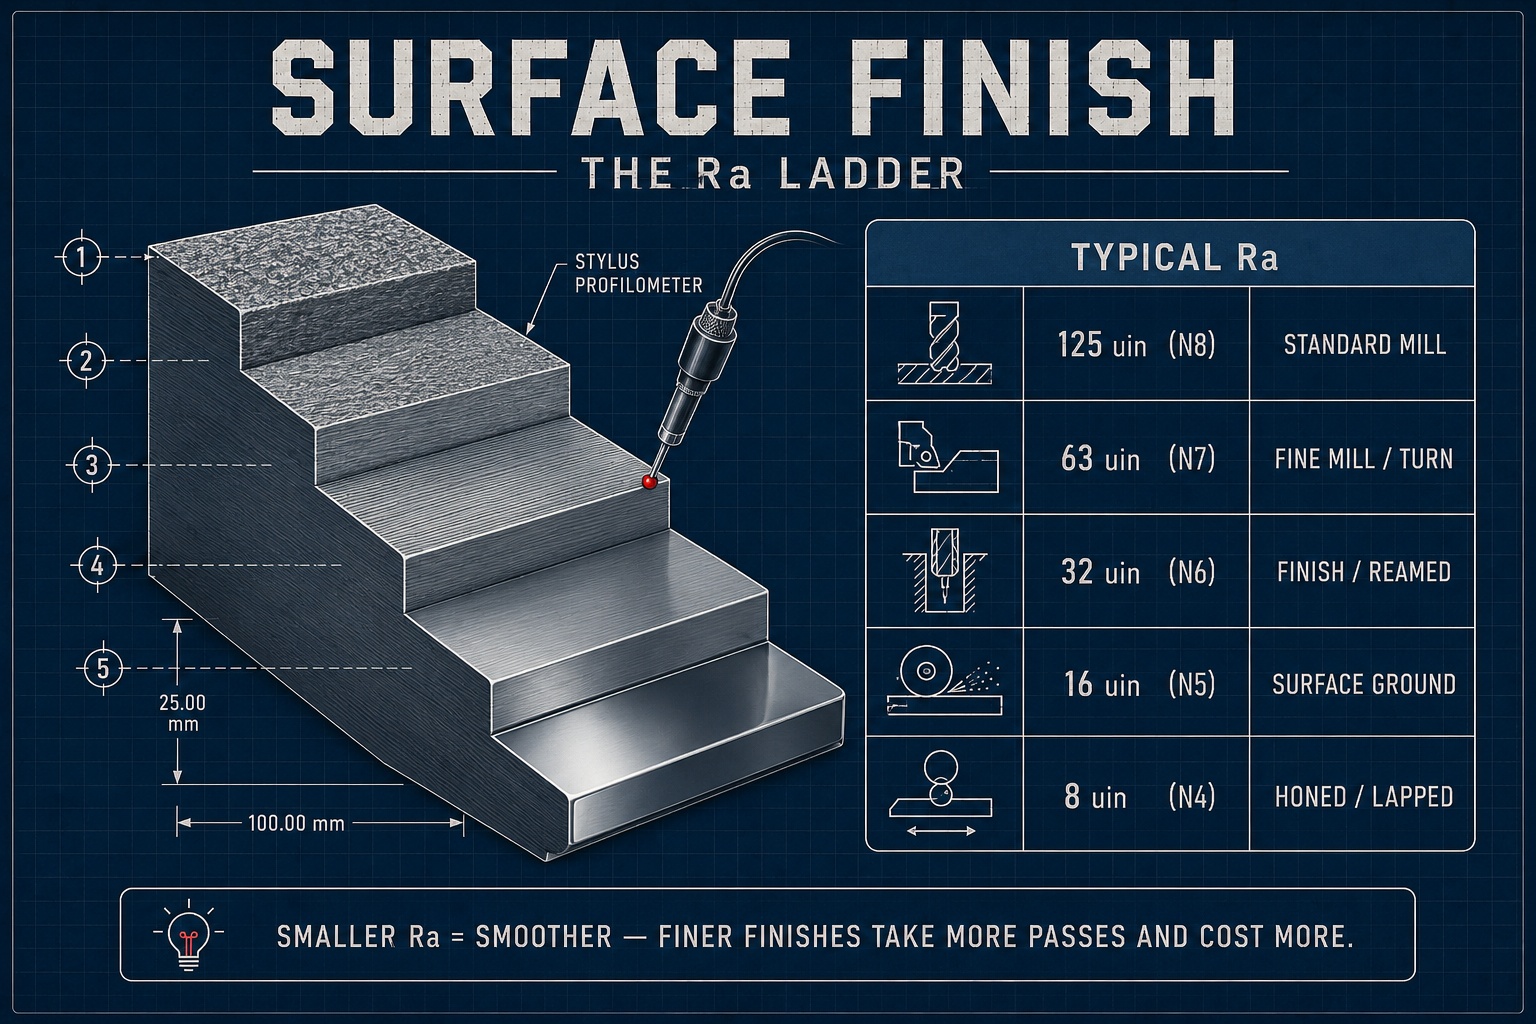
The chart below ladders the standard Ra values, the processes that achieve each rung, and what the surface actually looks like. µin (microinches) on the left, µm (micrometers) in parens.
Interactive Reference
Surface Roughness Visualizer
Surface textures and candidate processes are illustrative. Ra alone does not establish appearance, tactile feel, sealing performance or manufacturing cost.
Tap a preset, or pick any finish on the ladder below.
Modern Ra is the arithmetic average (AA / CLA) of the profile, defined in ASME B46.1. Older U.S. drawings often called out roughness as RMS (root-mean-square, the same as Rq), which reads about 11% higher than Ra for the same surface (RMS ≈ 1.11 × Ra). So a legacy "63 RMS" callout is roughly equivalent to Ra 57 µin, not 63. When a print just says a number with no parameter, confirm whether it means Ra/AA or RMS before tightening the spec.
Default precision CNC finish. Achieved via high speed toolpath; smooth finish.
32 µ'' AA (Ra 0.8 µm / N6)
- As-cast
- Coarse sand blast
- Rough cast
- Hot rolled
- Sand blast
- Rough mill
- Bandsaw
- Standard mill
- Standard turn
- Hot finish
- Fine mill
- Fine turn
- Drilled
- Finish mill / turn
- Reamed
- Surface ground (rough)
- Surface ground
- Honed
- Fine turn (Swiss)
- Ground
- Honed
- Fine bore
- Lapped
- Honed (precision)
- Polished
- Super-finished
Ra (arithmetic average roughness) is the most common callout. Ra 32 µin = Ra 0.8 µm — useful conversion to remember. Other parameters (Rz, Rt, Rmr) measure different things and are specified when Ra alone is insufficient.
Symbol key: the triangle marks are an obsolete, approximate drawing callout for machined finishes — from ▽ (roughest machined) to ▽▽▽▽ (lapped / polished). It's a four-class system, so each mark spans a band of Ra values and repeats across several rows; a genuinely as-cast or otherwise unmachined surface carries no triangle. Modern drawings specify the Ra value directly.
When to specify what
Pick the right rung for the job.
Non-functional surfaces
Backsides, hidden faces, internal cavities. Save the budget for surfaces that matter.
General machined
Most non-cosmetic, non-mating surfaces. Achieved with standard finishing pass.
Mating & sealing surfaces
Possible mating-surface example; the actual seal, lay and functional requirements govern.
Bearing surfaces, fluid
Possible sliding-surface example; verify the mating material, lubrication and texture specification.
Precision mating, optical mounts
Surface ground or honed. Cost steps significantly here — avoid unless required.
Lapped or polished
Fine-finish example, not optical, pressure-sealing or implant qualification. The complete surface specification governs.
Cost
Potential additional operations.
Cost doesn’t scale linearly with surface finish — it steps each time the process changes. Going from 125 µin to 32 µin is mostly free (same finishing pass). Going from 32 to 8 µin requires a different process (grinding or honing). 8 to 4 µin requires another (lapping or polishing). Plan around the steps.
250 → 32 µin
Single CNC operation
Roughing → finishing pass
32 → 8 µin
Add grinding or honing
Separate setup, separate machine
8 → 4 µin
Add lapping
Often per-part hand operation
4 → 1 µin
Add polishing
Specialist labor — quote each part
Molding Specs
CNC to RMA / ARPM Mold Finish
For molded rubber and elastomer products, mold cavity surface quality is governed by Association for Rubber Products Manufacturers (ARPM, formerly Rubber Manufacturers Association or RMA) standards. Mold machining and F1/F2 polishing, lapping and buffing require a process plan agreed with the machining and finishing suppliers.
Fine CNC pass + multi-stage diamond hand polishing / lapping (coordinated with finishing partners)
Mirror-like, completely uniform, free of tool marks, scratches, or nicks.
Ultra-glossy, highly cosmetic, premium consumer-facing elastomer surfaces.
Finish CNC pass (Ra 32) + buffing to remove micro-scallops (coordinated with finishing partners)
Polished steel mold finish. Very small, barely visible machine tool marks may remain.
Semi-glossy, highly uniform, clean sealing or sliding interface elastomer surfaces.
Standard CNC rough/finish milling or turning (Ra 63–125). No polishing.
Typical machining tool marks and height-step scallops are fully visible.
Matte, non-cosmetic industrial rubber seals, gaskets, or internal bushings.
Standard CNC machining + sand or glass-bead media blasting
Uniform textured satin/matte. Masked to ensure clean parting lines.
Fine-textured, grip-oriented, micro-matte rubber parts with no glare.
Design Tip: While F1 & F2 yield highly aesthetic parts, they require intense manual mold polishing, multiplying mold lead times and tooling costs. F3 (Commercial) is the industry default—specify it for all non-sealing and non-aesthetic rubber surfaces.
Specifying tips
Three things that make finish callouts cheaper.
Apply finish only to surfaces that need it
Use directional surface callouts on the drawing. A blanket 'all over' callout treats every face as critical.
Loosen what doesn't serve a function
Bottom of pockets, internal walls, non-mating shoulders — most can run at 125 µin or as-machined.
Beware combined callouts
Specifying both Ra AND Rz, or Ra at multiple lay directions, multiplies inspection time. Pick the parameter that drives the function.
Keep exploring
Related tools & references
Convert between Ra, Rz, RMS, and N-grade callouts.
How finish callouts interact with dimensional tolerance.
What each step toward a finer finish adds to part cost.
How feed per tooth drives the milled and turned Ra you can hit.
Which operations reach which finish ranges.
Not sure what surface finish to specify?
Tell us about your part and we'll get back to you promptly. Aerospace, medical, defense, and semiconductor production work welcome.Email CAD models and drawings to sales@digitalmachine.com, including ITAR, EAR, CUI and AS9100 work. Keep controlled technical data out of web forms.
First articles through full production runs