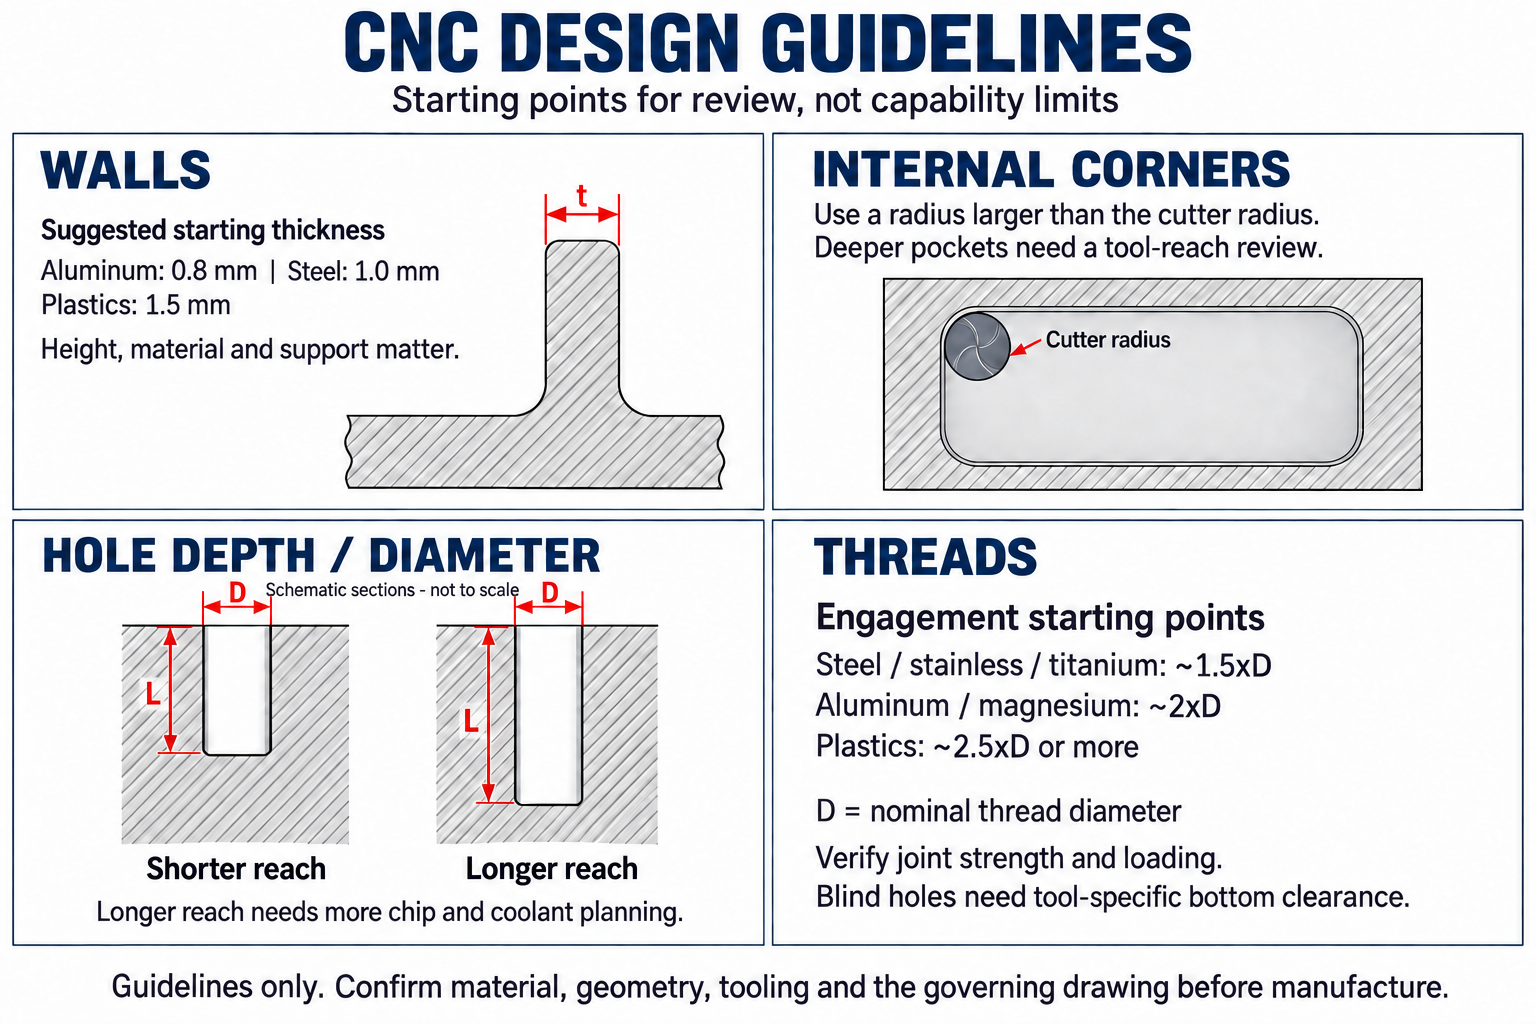
FIELD GUIDE 01
Pockets & tool access
Give the cutting edge room to reach, clear chips and leave the required corner.
Pockets & tool access
Give the cutting edge room to reach, clear chips and leave the required corner.
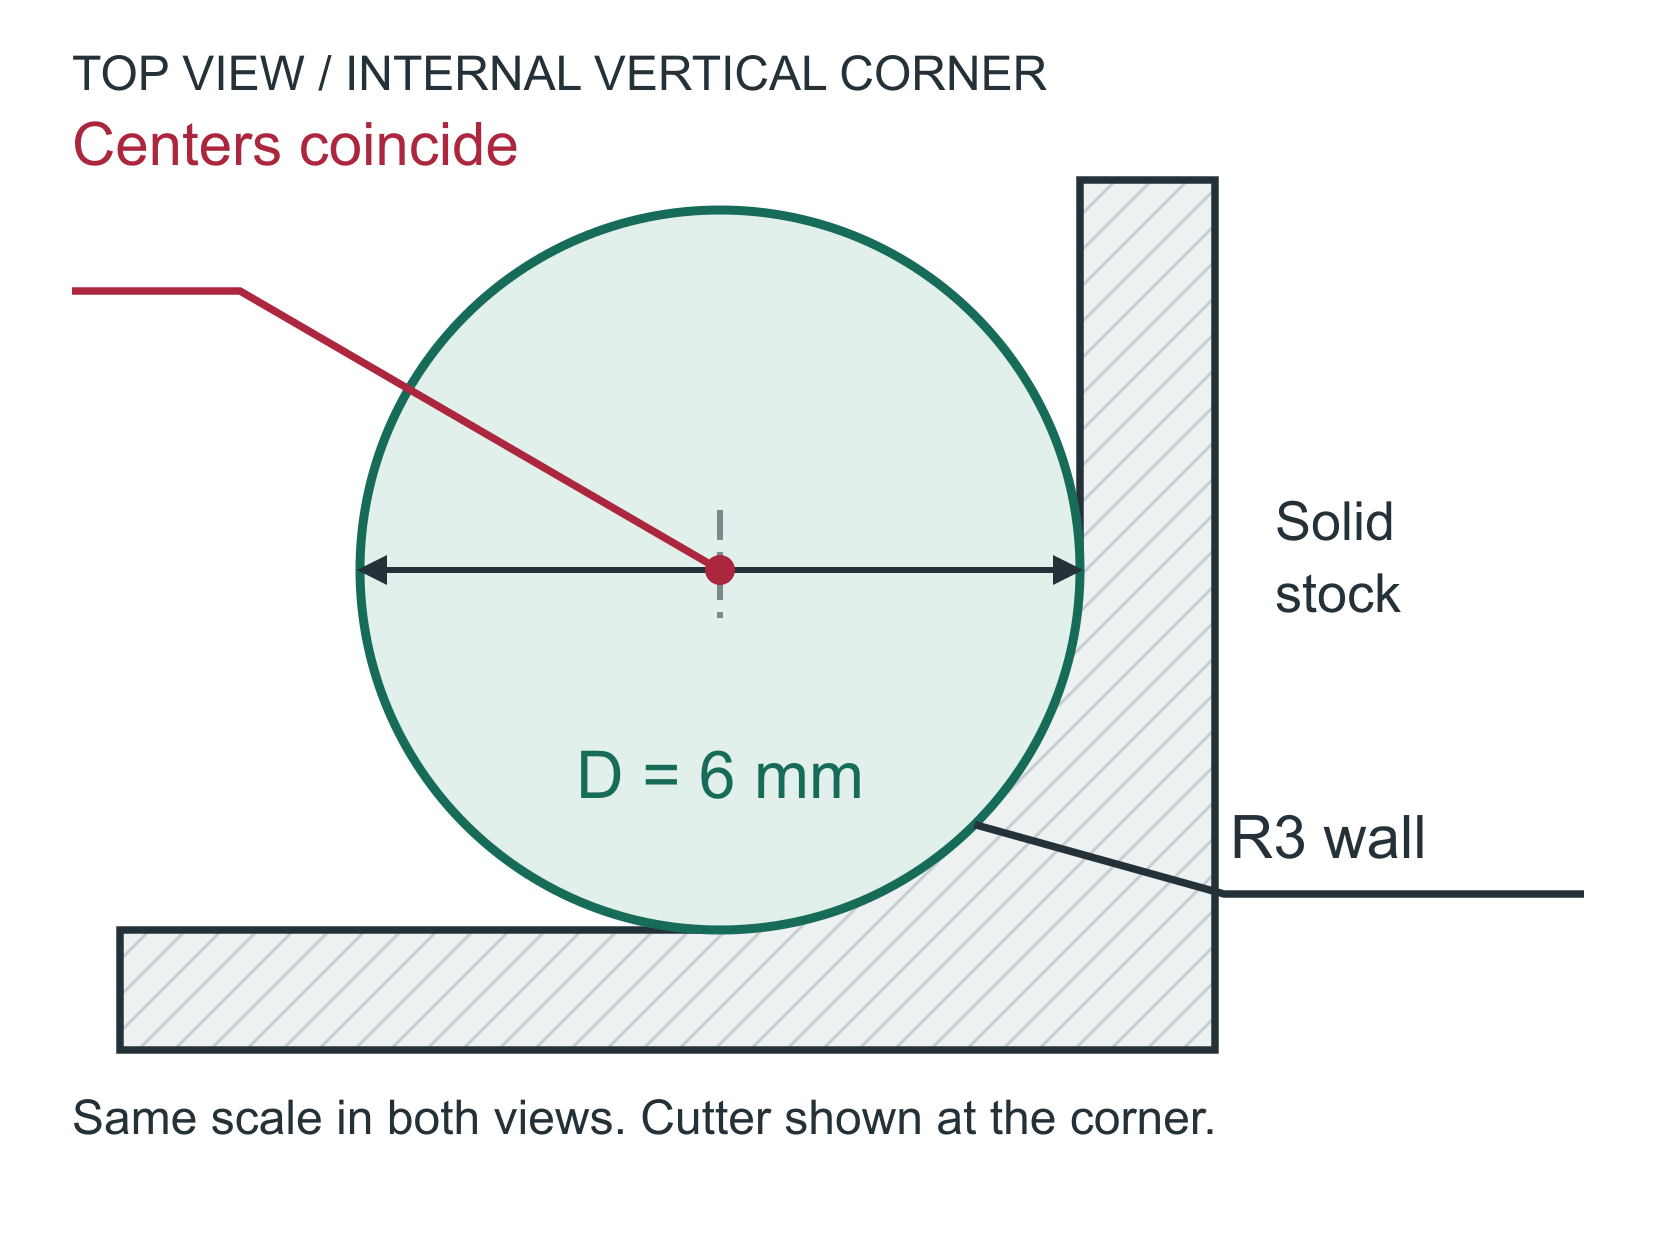
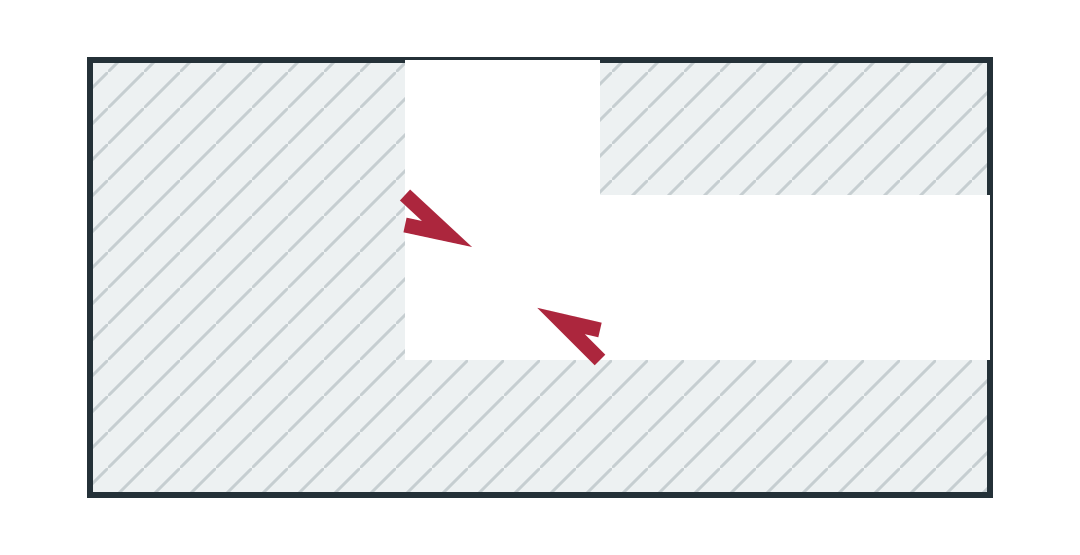
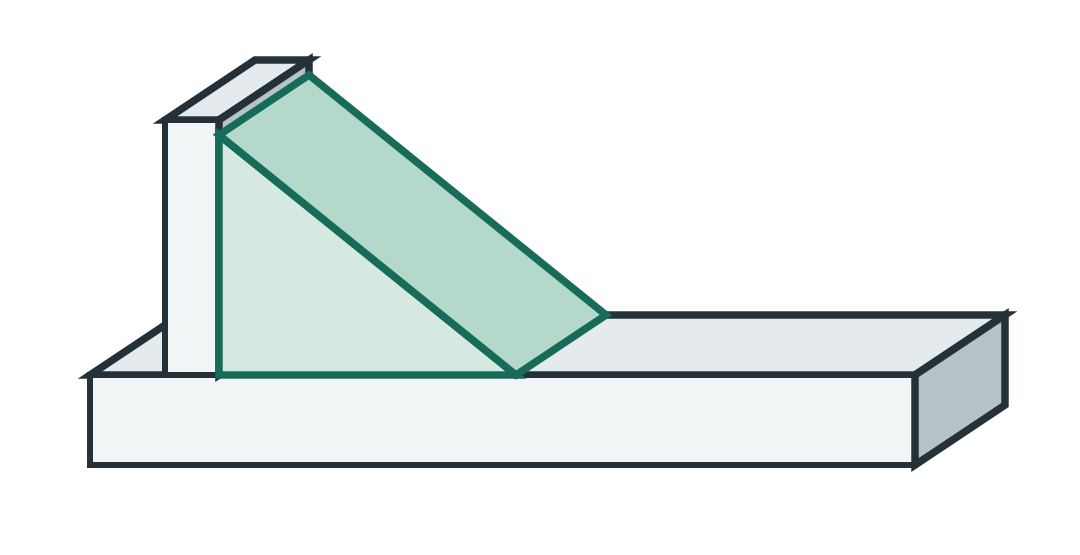
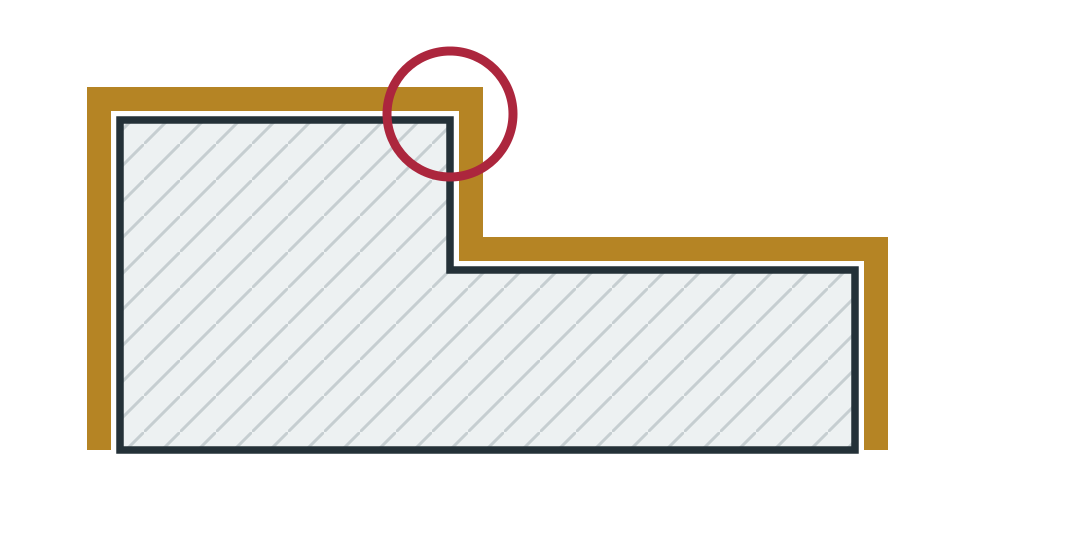
R3 corner / diameter 6 cutter
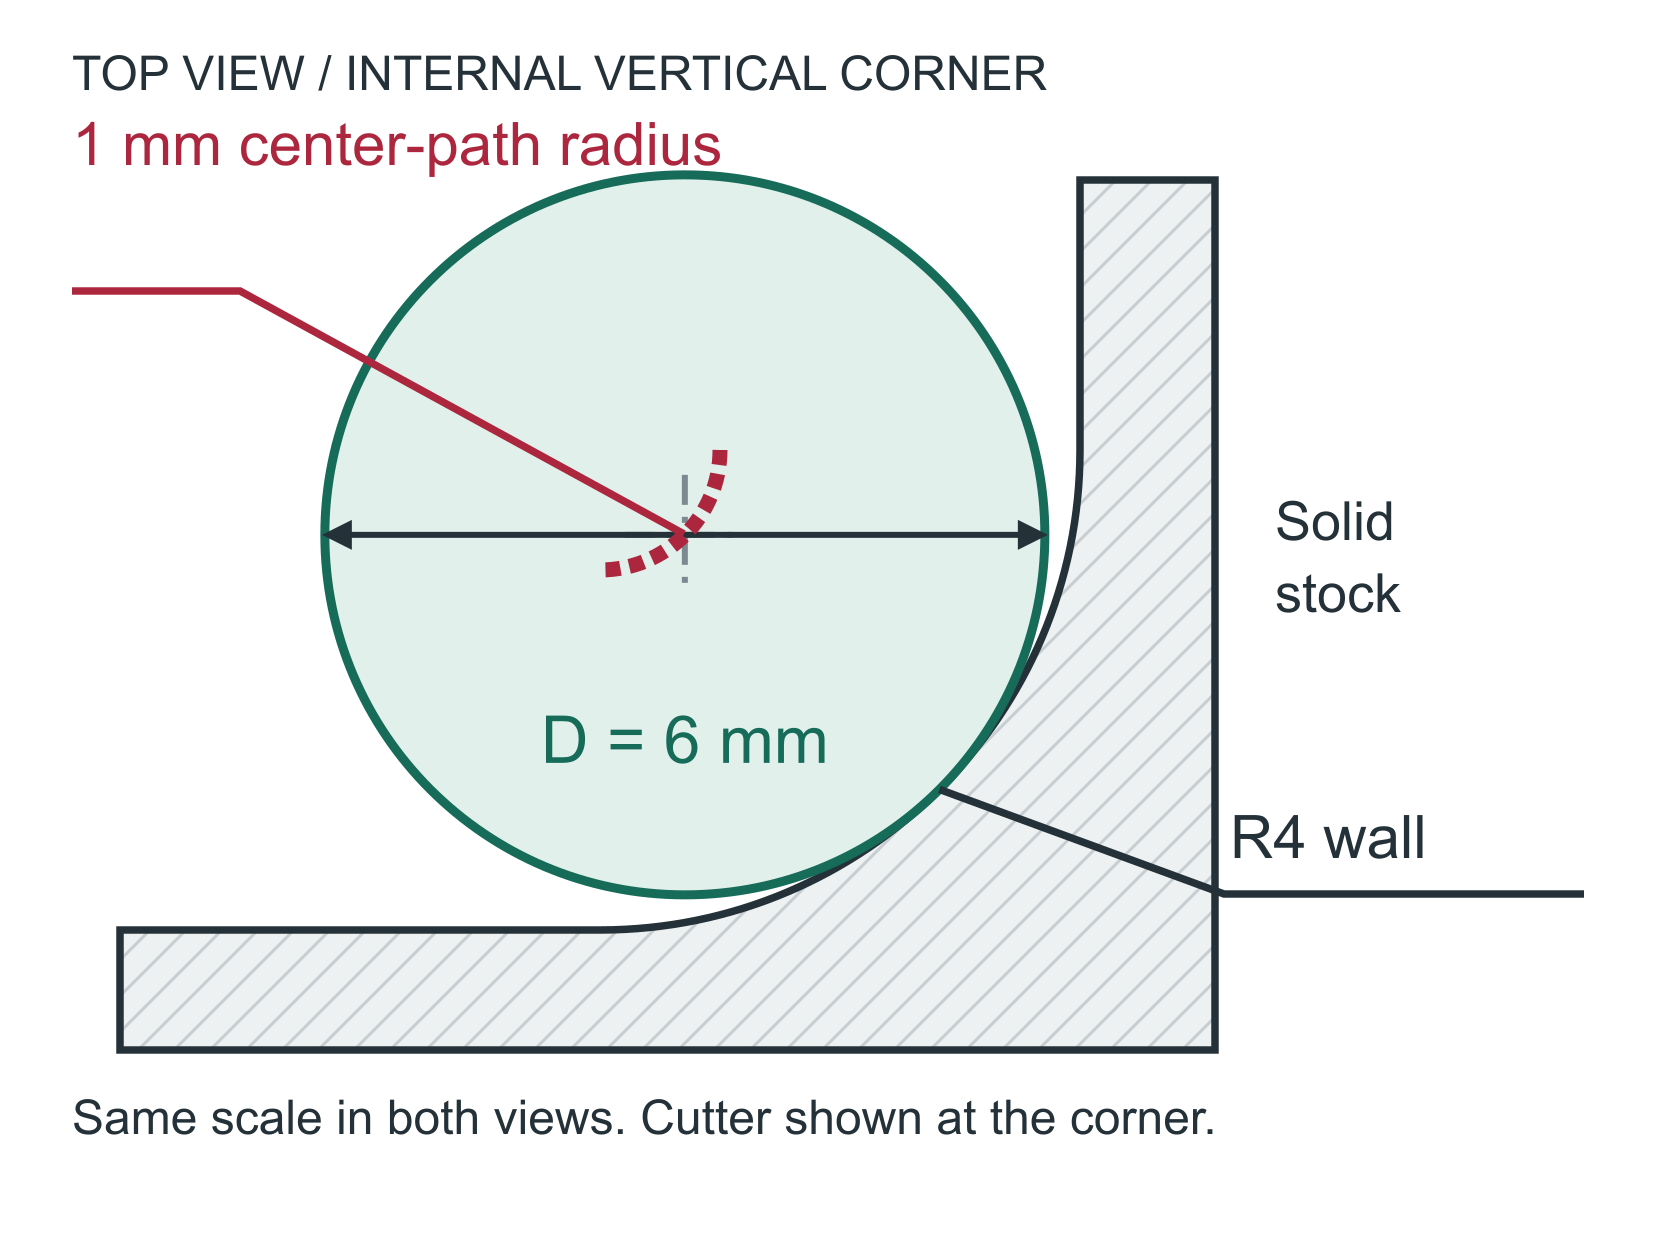
R4 corner / diameter 6 cutter
Corner-path radius = R - D/2
R3: 3 - 6/2 = 0 mm | R4: 4 - 6/2 = 1 mm03Reduce unnecessary reach
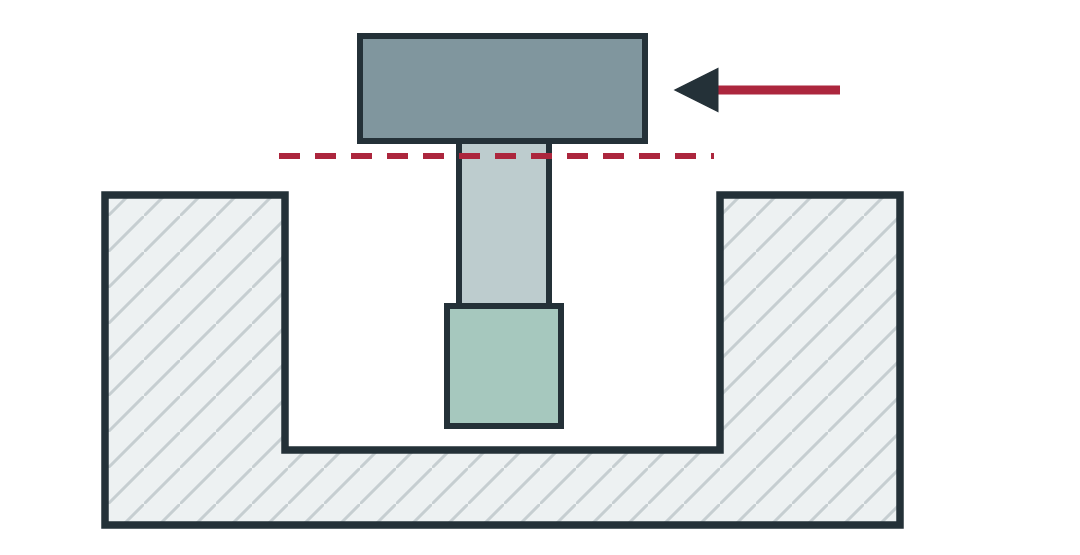
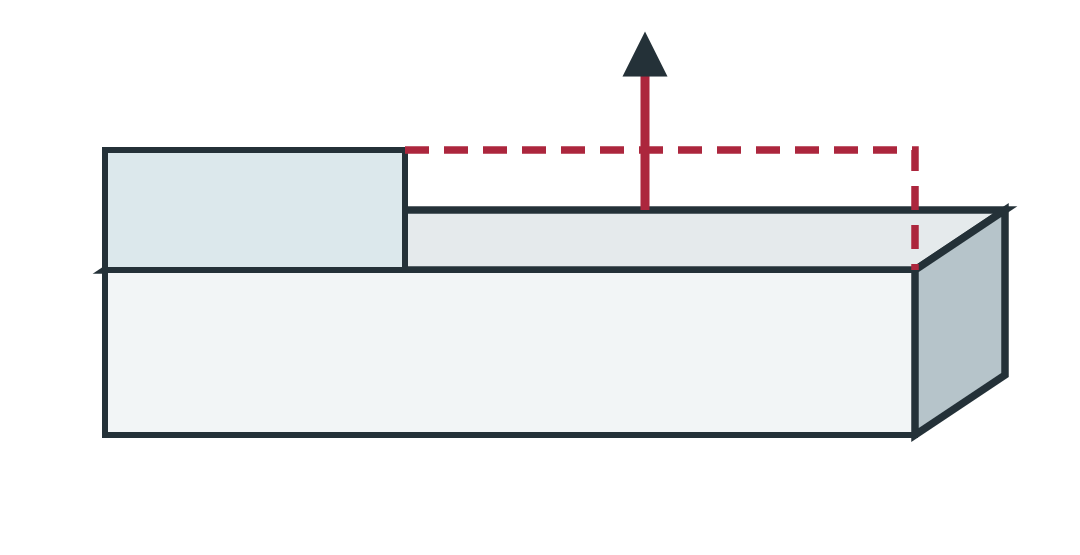
Flutes provide chip space; the neck and holder also need clearance. A deep pocket may require a long, less rigid tool.
CAD: keep nonfunctional pockets shallow.
04Clear square mating corners
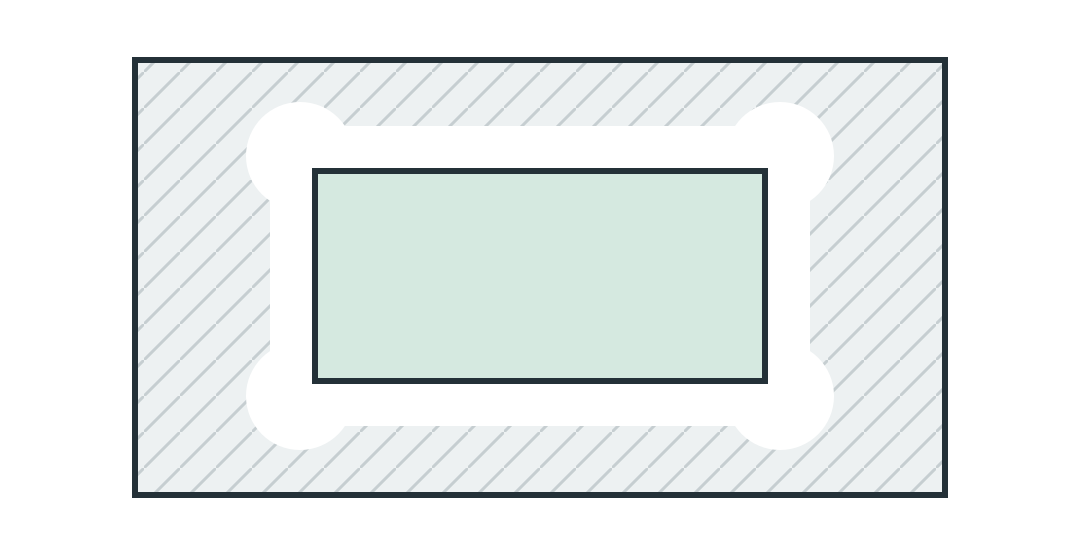
A round tool leaves an inside radius. Local corner relief can clear a square insert; verify fit and the remaining load-bearing section.
CAD: add relief only where permitted.
05Plan the tool approaches
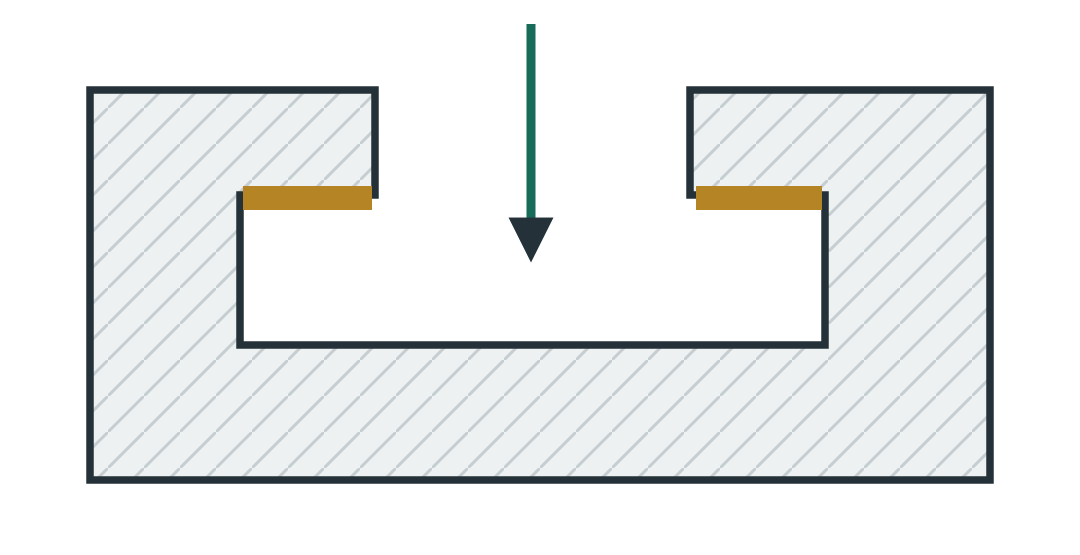
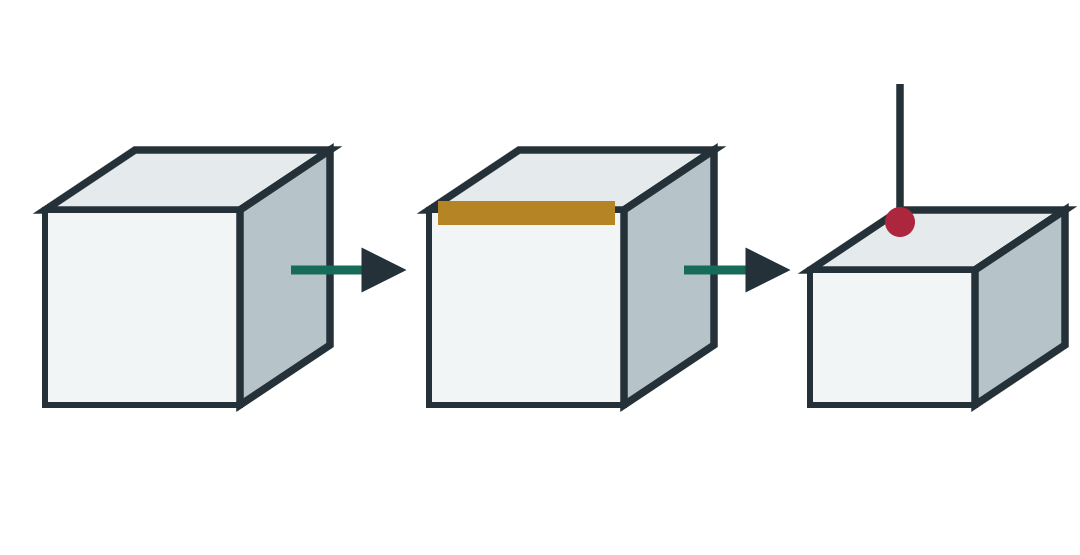
Group accessible features where function permits. Re-clamping adds handling; undercuts still need a tool entry and exit path.
CAD: review access and necessary setups early.
06Distinguish blind and through
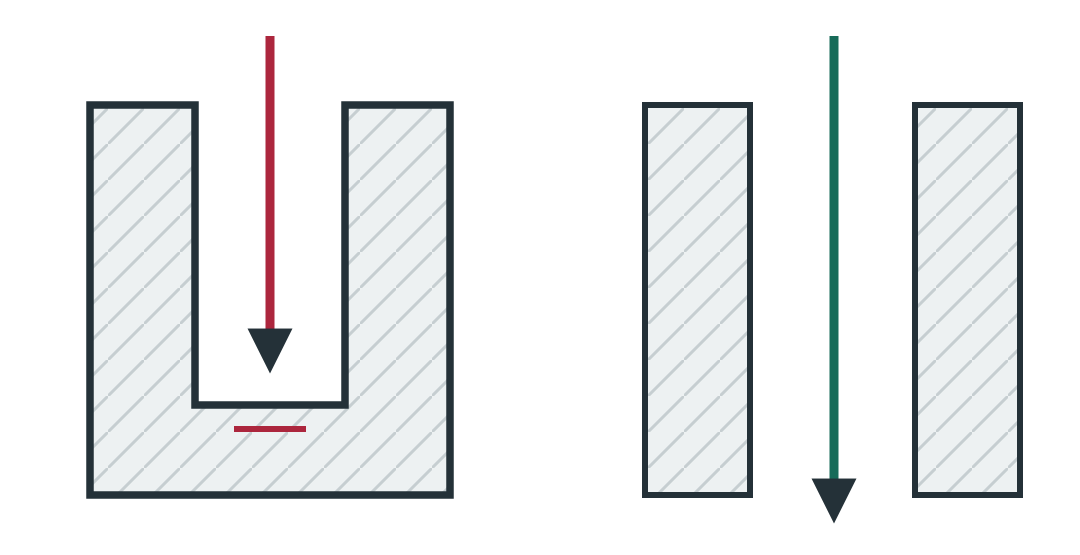
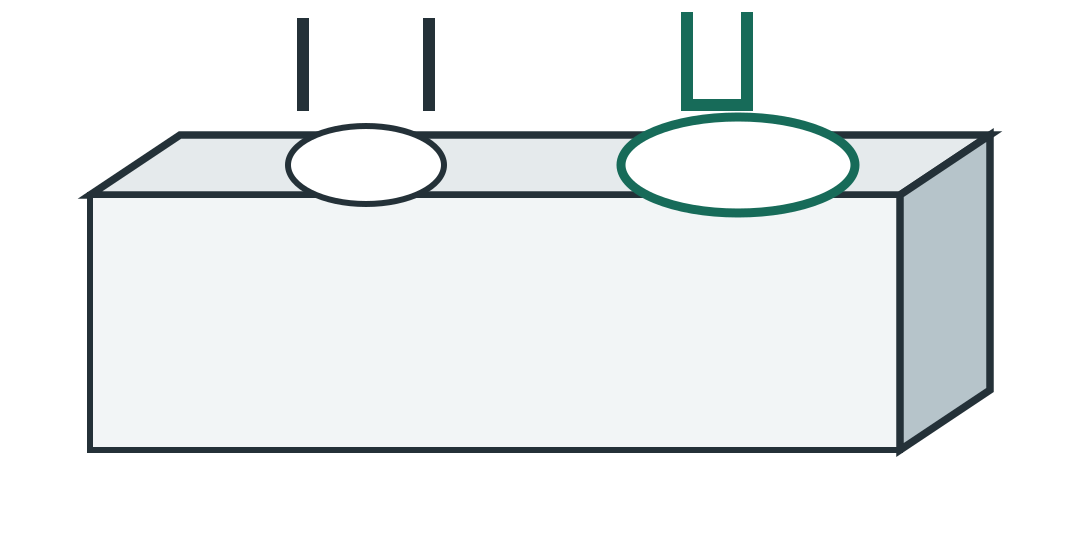
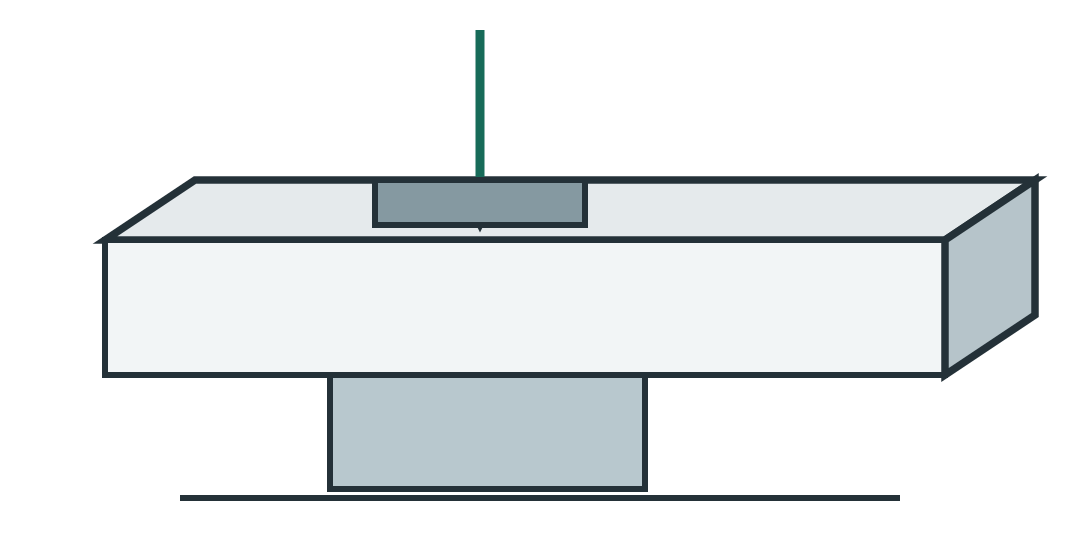
Wire EDM needs a through path in conductive material and wire entry. A blind floor needs another approach, such as sinker EDM.
CAD: preserve required floors and sealing walls.
A larger corner helps the toolpath; it does not prove tool reach. Check flute, neck and holder clearance separately.
BEFORE RELEASE Protect fit, loads, sealing and required material sections when changing geometry.
- Identify the smallest internal vertical radius.
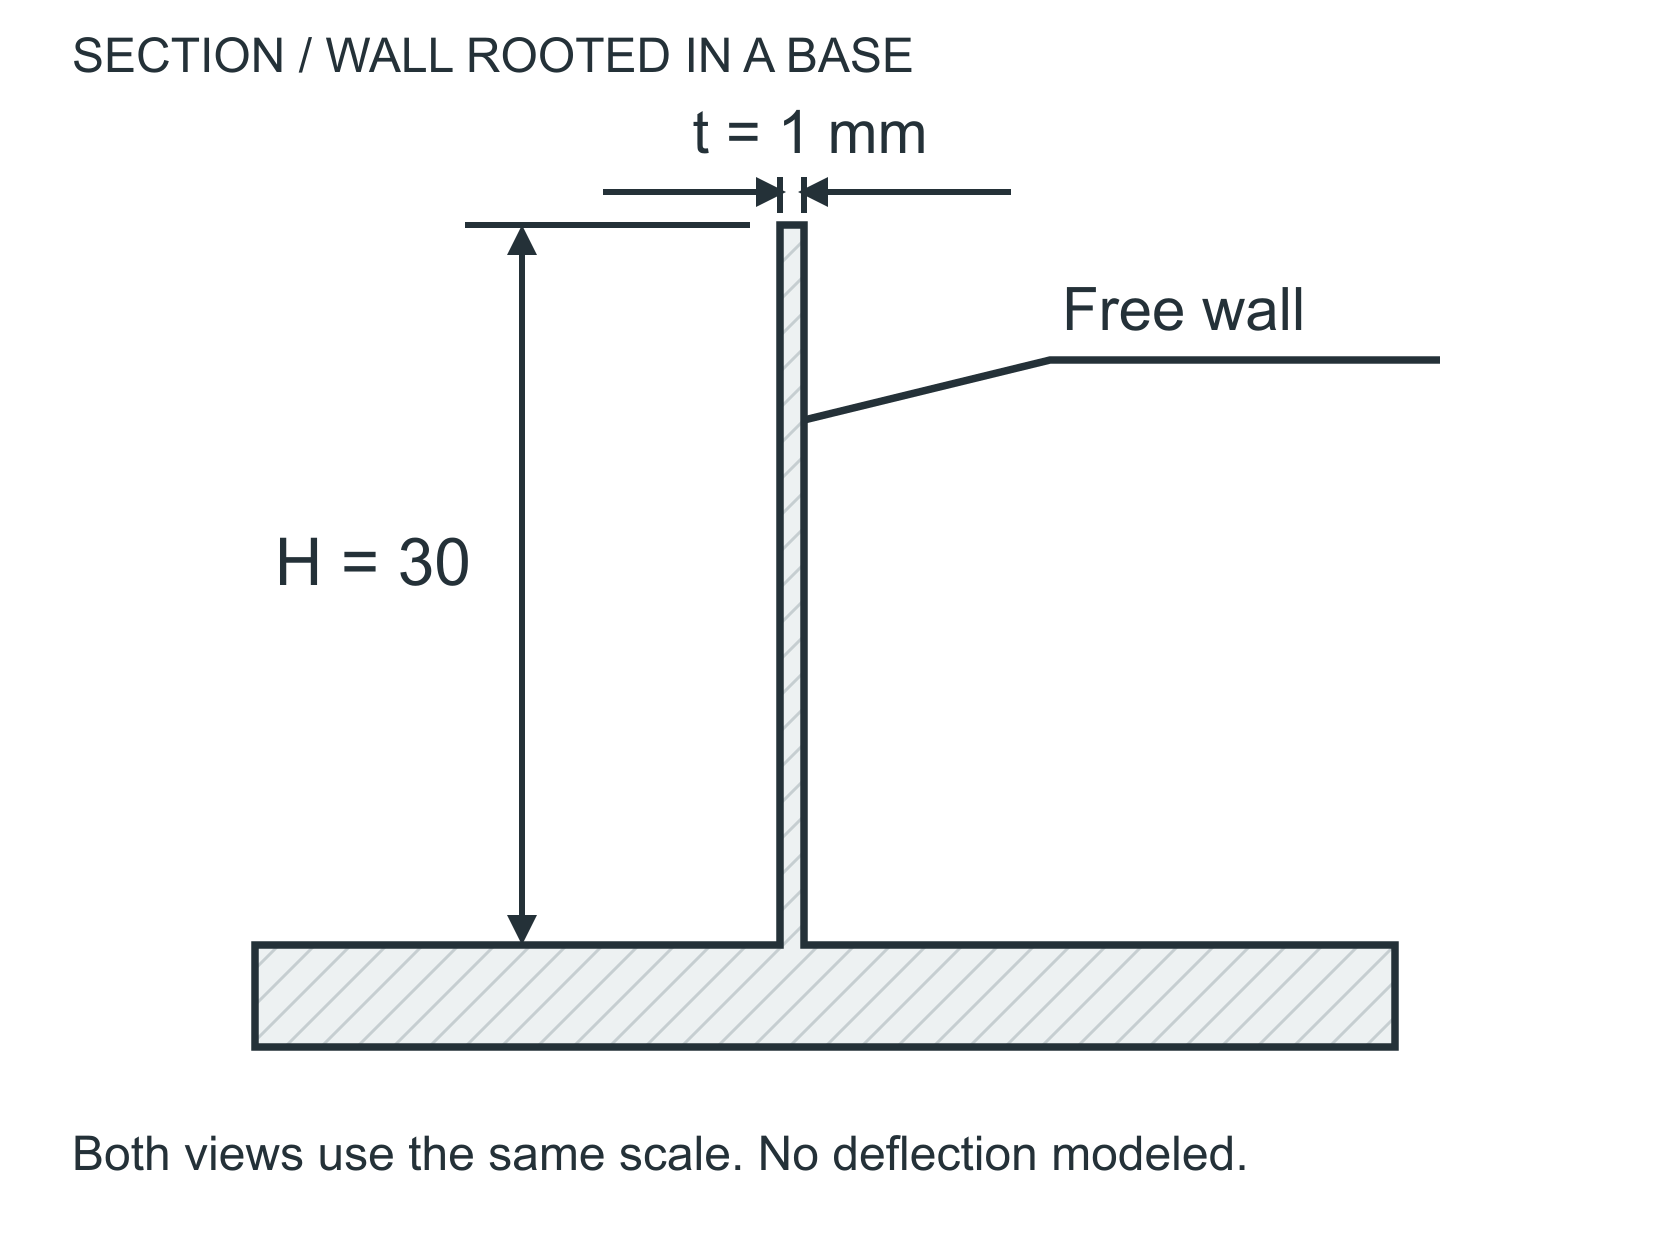
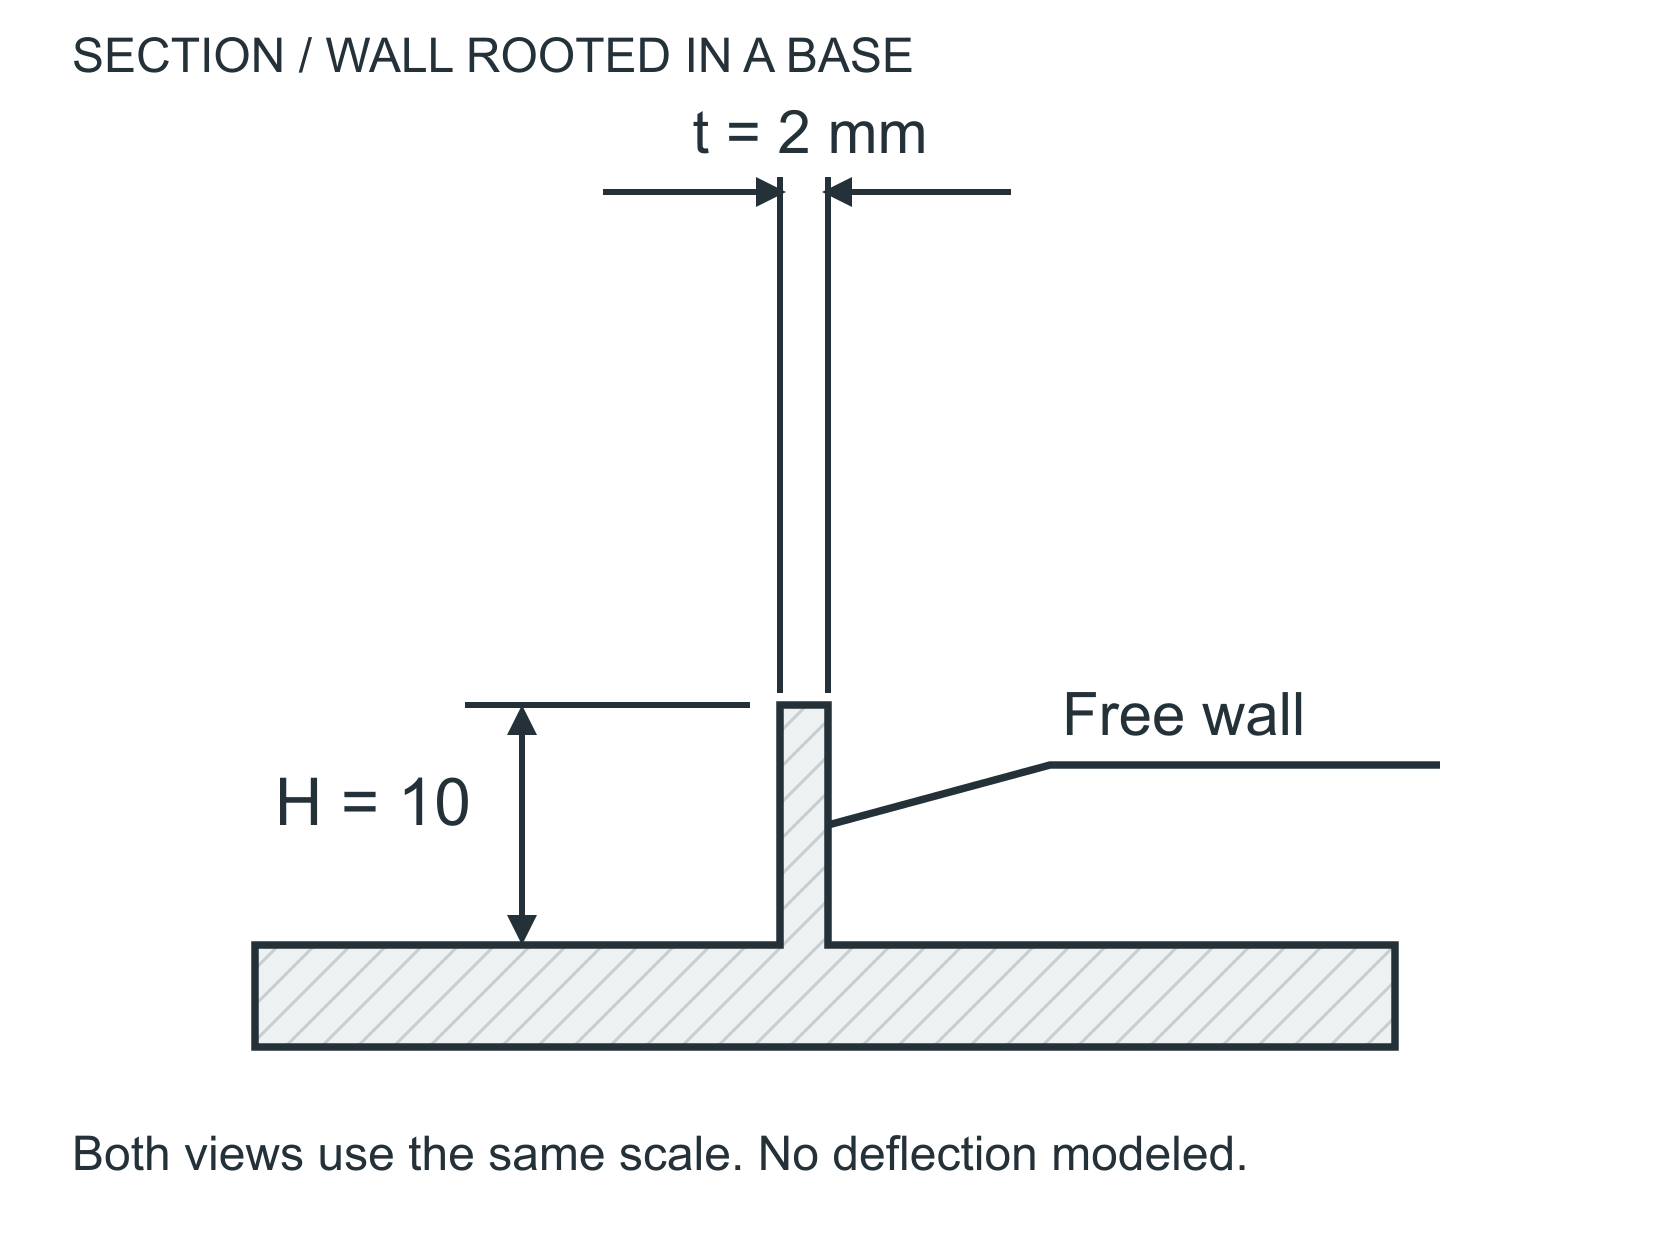
- Dimension pocket depth separately from wall height.
- Check tool and holder access to every feature.
- Identify square-corner mating requirements.
- Mark any permitted corner relief on the drawing.
- Discuss inaccessible undercuts before release.
More design context & checklist
Same 24 mm pocket depth. A 6 mm cutter in an R3 corner has zero radius clearance; R4 gives 1 mm. Depth / cutter diameter remains 4:1 in both cases. This is geometry, not a reach approval. Illustrative geometry, not a production drawing.
- Corner clearance
- A larger internal vertical radius gives the cutter room to sweep through the corner. Verify the mating part before changing it; a functional sharp corner may need relief or another process.
- Reach is not just depth
- Check flute length, relieved neck, holder diameter and adjacent walls. A cutter can reach the floor while its holder still collides with the part.
- Process boundary
- Wire EDM needs an accessible through-cut in conductive material. A blind pocket requires a different approach; do not specify wire EDM simply because a corner is square.
In any alloy, long tools and unsupported walls need joint review. Hardness, tool geometry and cutting conditions change the workable envelope; no universal L/D ratio establishes capability.
Review prompts only; checks are not stored or sent and do not constitute approval.